 EN

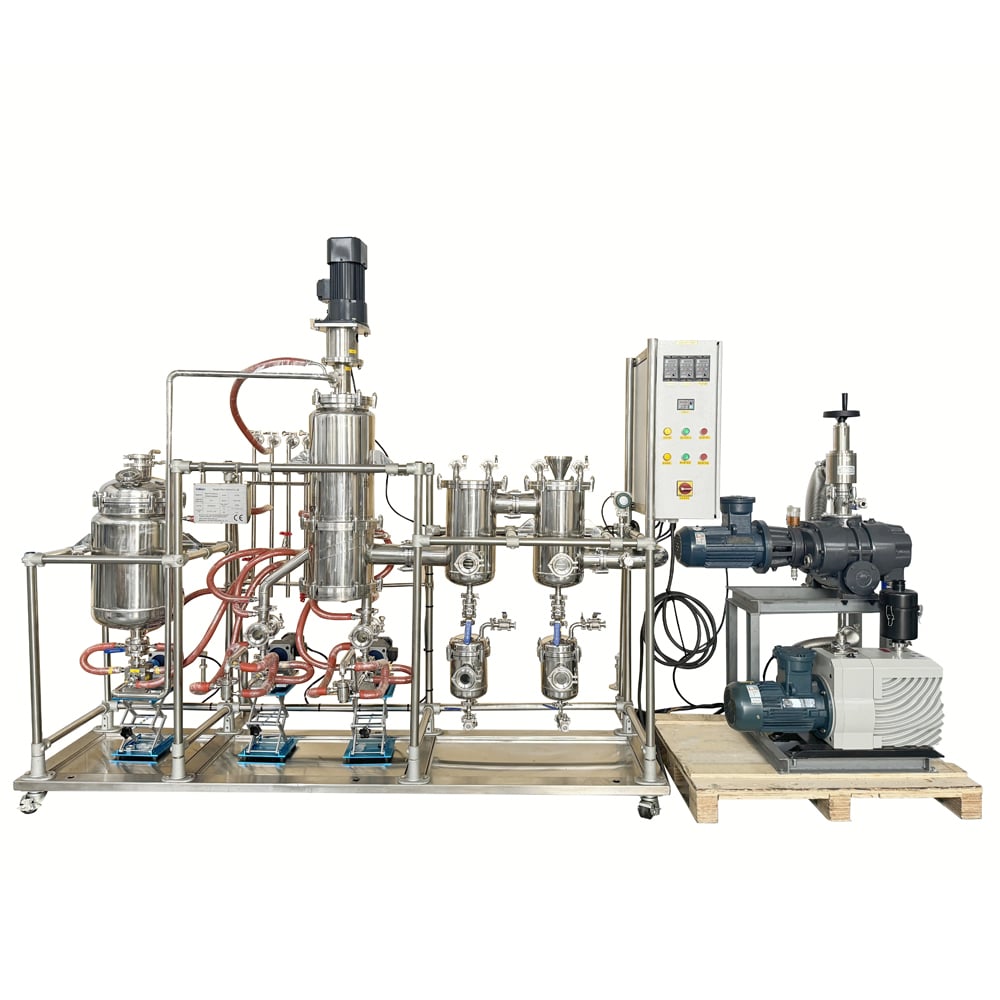
The wiped film evaporator has become an indispensable technology across pharmaceutical, chemical, food, and specialty manufacturing industries. Processing professionals recognize that a wiped film evaporator delivers superior thermal efficiency, gent...
VIEW MORE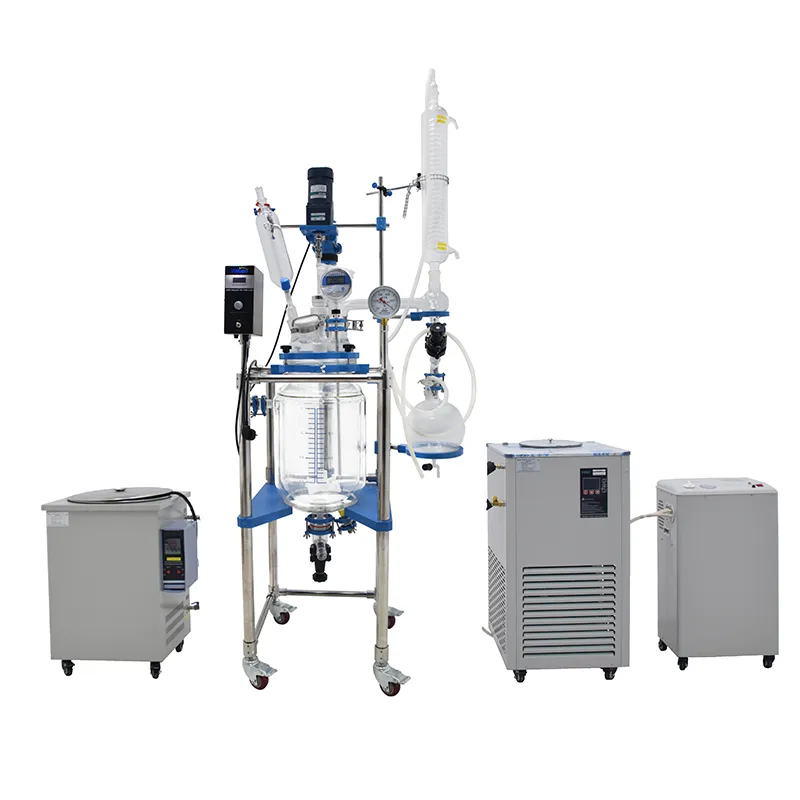
Fine chemical production demands precision, control, and scalability from concept to commercial viability. A pilot scale reactor bridges the critical gap between laboratory research and full-scale manufacturing by providing a controlled environment w...
VIEW MORE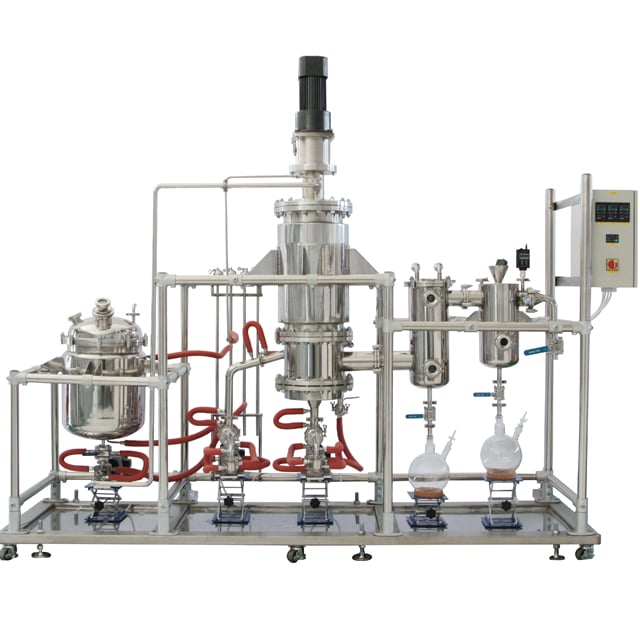
Selecting the right Wiped Film Evaporator is a critical engineering decision that directly impacts your separation process efficiency, product quality, and operational costs. Engineers working in chemical processing, pharmaceutical manufacturing, foo...
VIEW MORE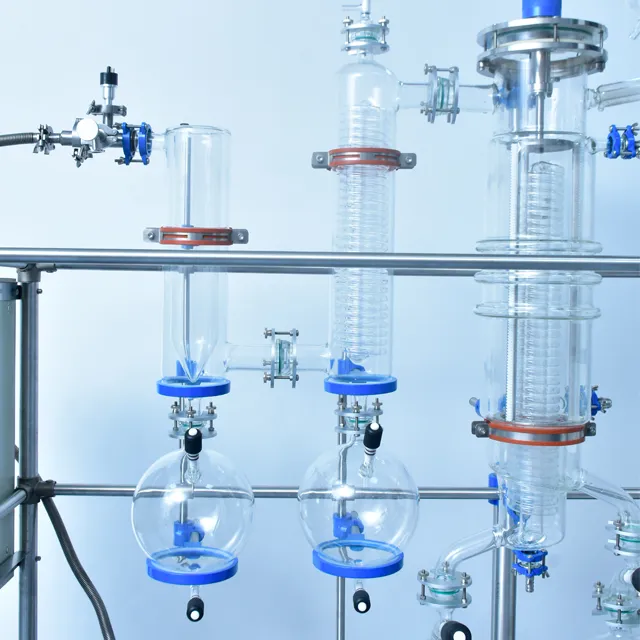
Selecting the right Distillation System for heat-sensitive materials is one of the most critical decisions in pharmaceutical, botanical, and specialty chemical processing. Heat-sensitive compounds—including essential oils, cannabinoids, vitamin...
VIEW MORE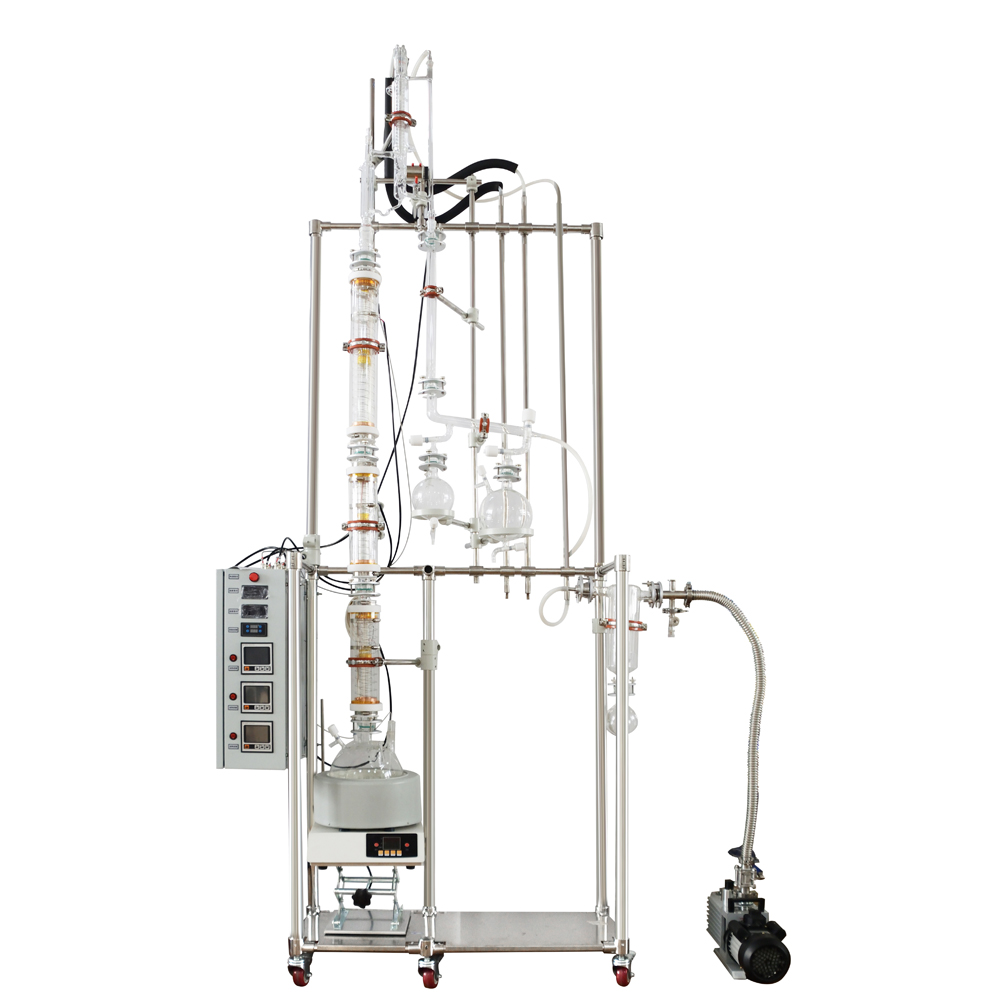
Designing an effective distillation setup for essential oils and natural extracts requires careful planning, technical knowledge, and attention to multiple interconnected factors. A properly engineered distillation setup determines the quality, yield...
VIEW MORE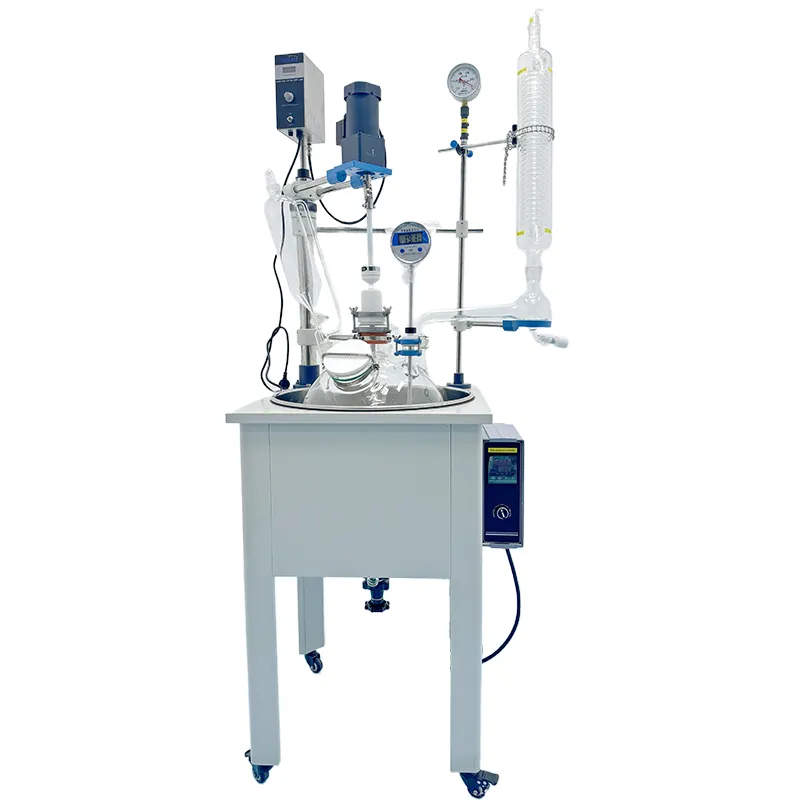
Exothermic chemical reactions release significant heat energy during processing, making them inherently challenging to control safely. A properly designed reactor must incorporate multiple safety layers to prevent thermal runaway, equipment damage, a...
VIEW MORE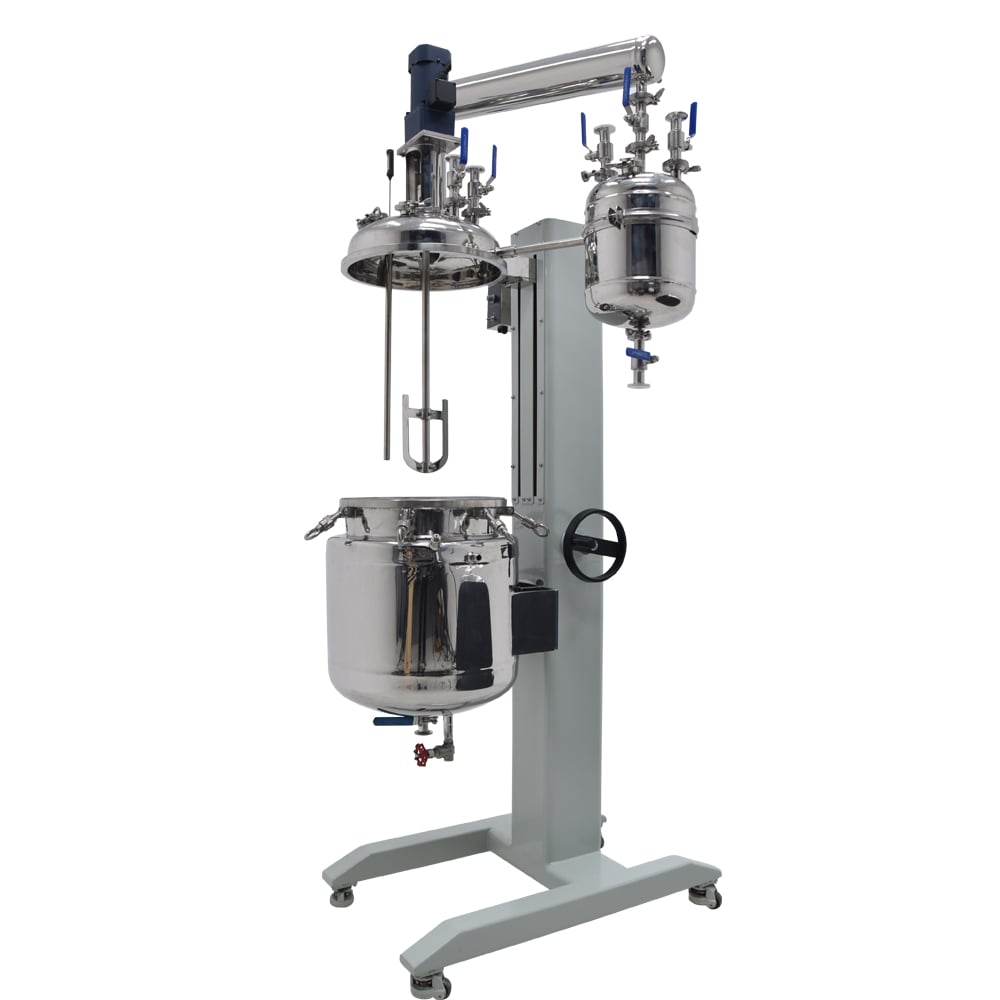
Stirring speed is one of the most critical operational parameters that directly influences how reactions progress inside a chemical reactor. The rate at which a chemical reactor mixes its contents determines not only reaction uniformity but also heat...
VIEW MORE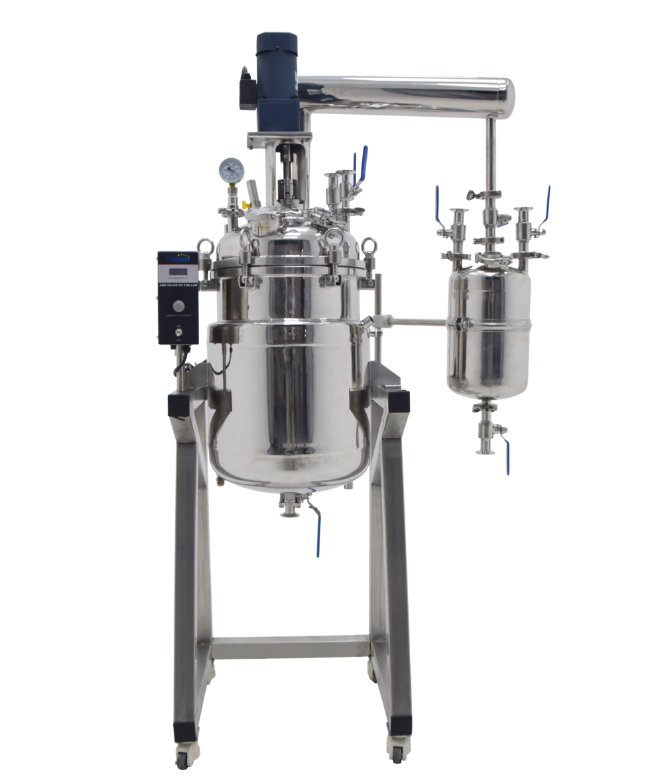
A chemical reactor is the heart of any modern chemical manufacturing facility, where precise temperature management directly impacts product quality, yield, and safety. Understanding the available heating methods for a chemical reactor is essential f...
VIEW MORE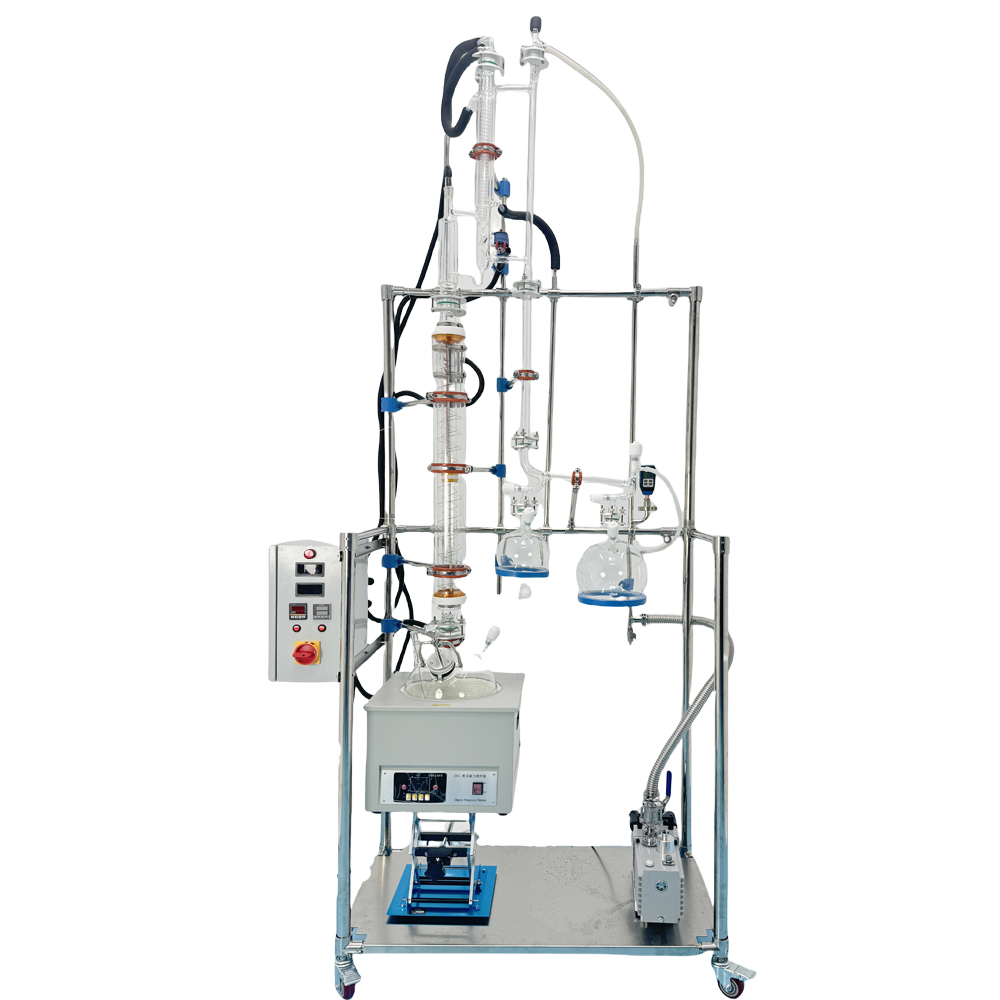
A distillation reactor represents a significant advancement in chemical processing technology by merging two critical operations into a single integrated system. Traditional industrial workflows require separate equipment for reaction and distillatio...
VIEW MORE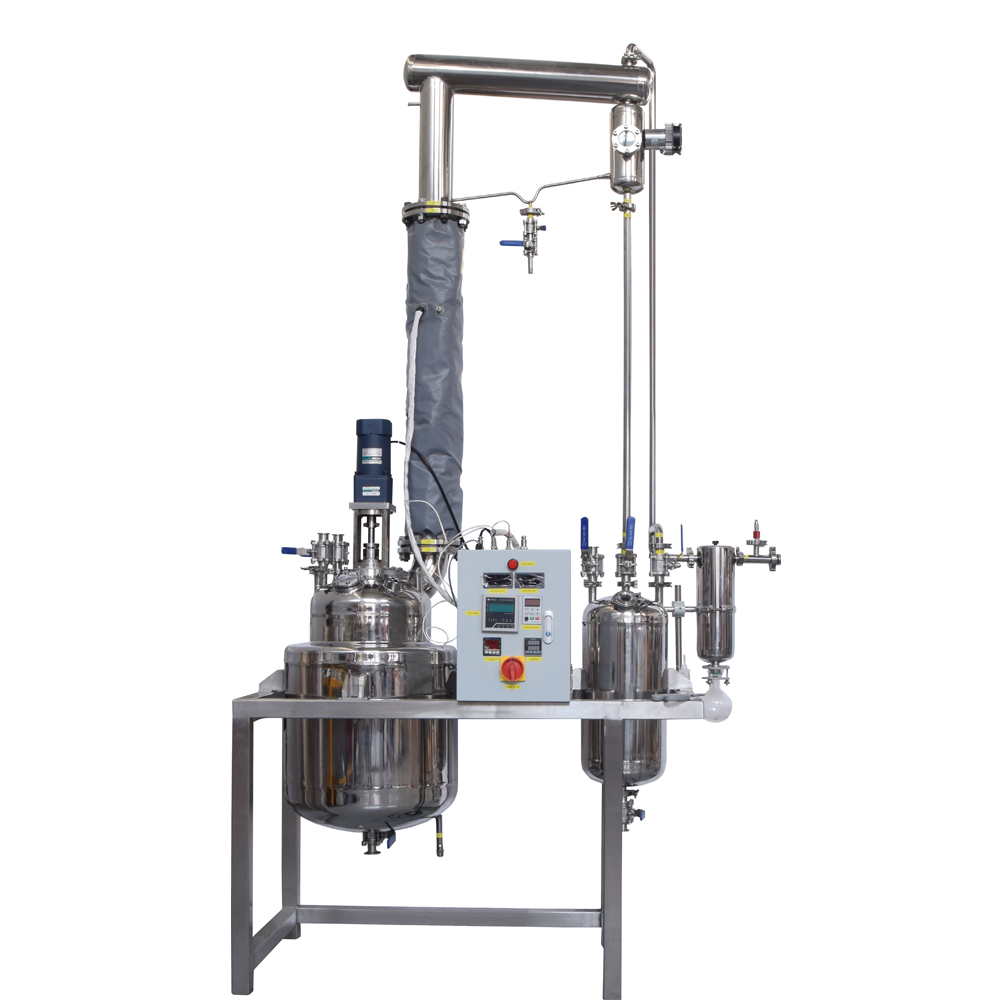
A rectification reactor represents a sophisticated advancement in chemical separation technology, designed specifically to enhance both the purity of separated components and the overall efficiency of distillation processes. In industrial application...
VIEW MORE
The performance of a rectification reactor directly impacts the quality and efficiency of separation processes in industrial applications. Understanding the factors that influence a rectification reactor's effectiveness is essential for operators, en...
VIEW MORE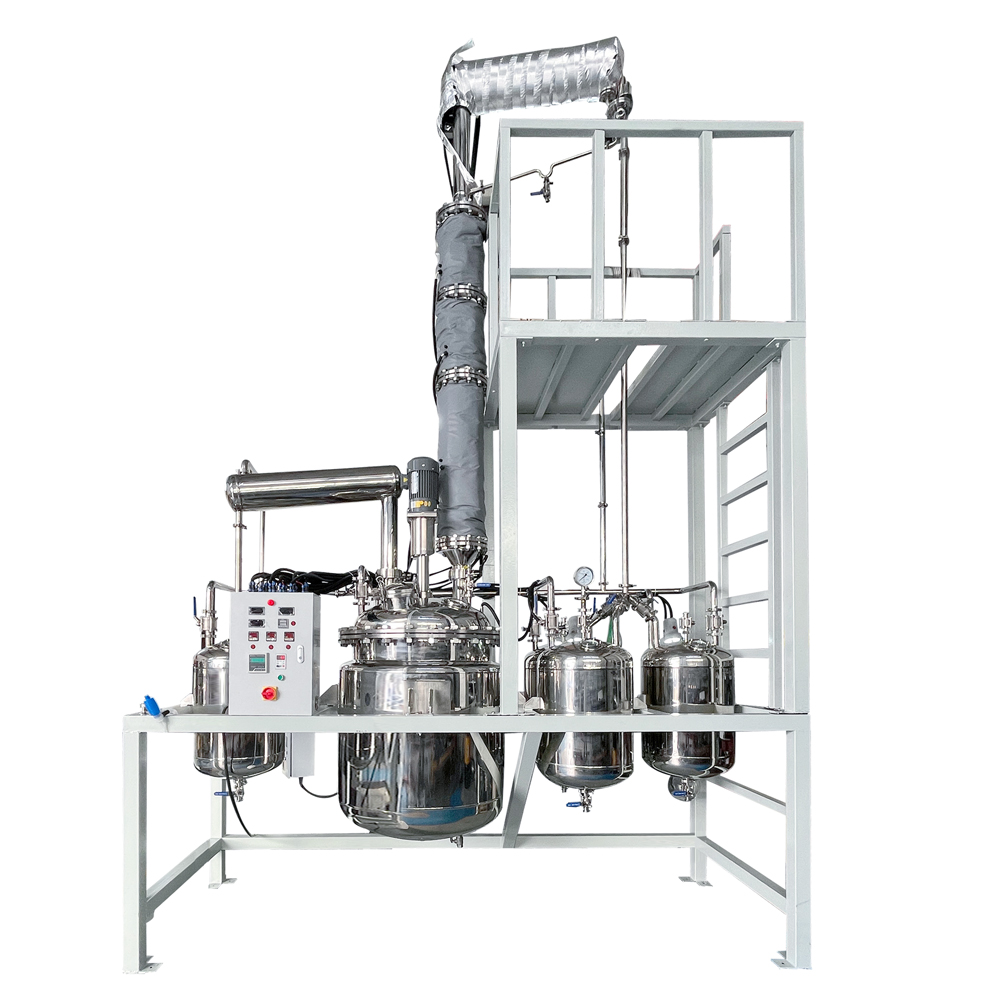
A rectification reactor plays a critical role in modern industrial separation technology by enabling precise control over distillation processes. This specialized equipment combines continuous fractionation with advanced heat management to achieve hi...
VIEW MORE